Like all hygroscopic materials, the water content of wood varies depending on the relative humidity of the environment in which it is located. During cold weather, the raw material in the timber industry is generally stored either outdoors, or in unheated rooms with high relative humidity. In processing areas, the relative humidity is usually lower. The interior fibres of the wood react to this change when moving between areas and can crack, deform, or significantly change in size, all of which causes a deterioration in value and a problem with productivity throughout the industry.
Ideally, the wood should usually contain 11% moisture content, which requires a storage area with an RH of 60%. This can be hard to achieve as it is unusual for a ducted air conditioning facility to be installed in either processing or storage areas.
To address these challenges, selecting an appropriate humidification system is key to controlling moisture exchange within the wood and preventing defects such as cracking, warping and dimensional instability during processing. A properly designed solution helps maintain consistent material quality and reduces losses caused by uncontrolled humidity variations.
Further guidance on how to choose the most suitable solution can be found in our article on the best humidifier for timber processing to prevent cracking and warping.


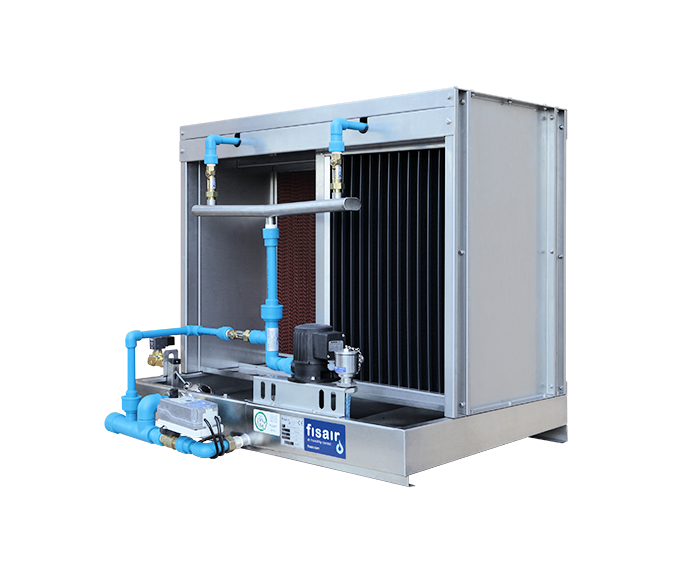 The most hygienic and efficient.Contact panel evaporative humidifiers, with the best performance on the market for efficiency at lower pressure drop and certified hygiene.


